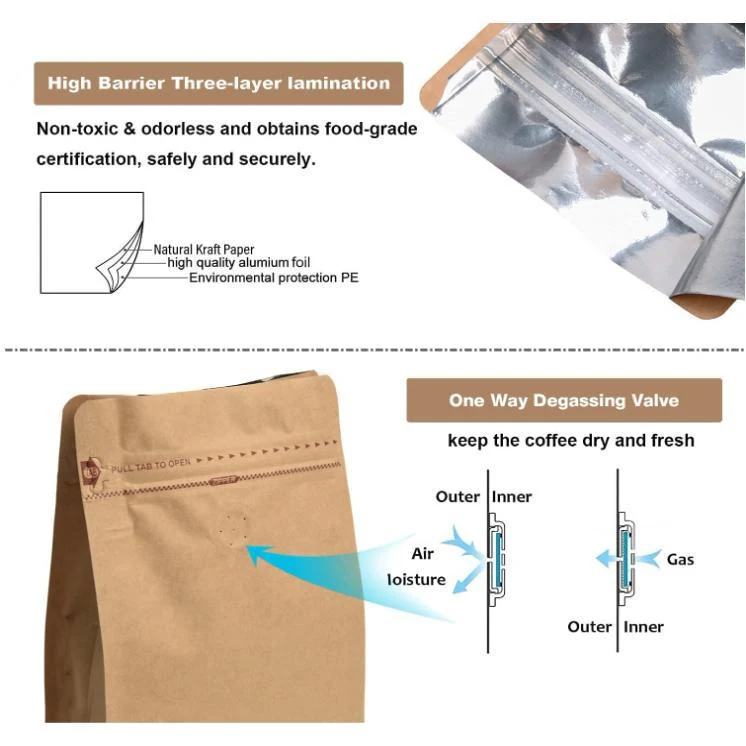
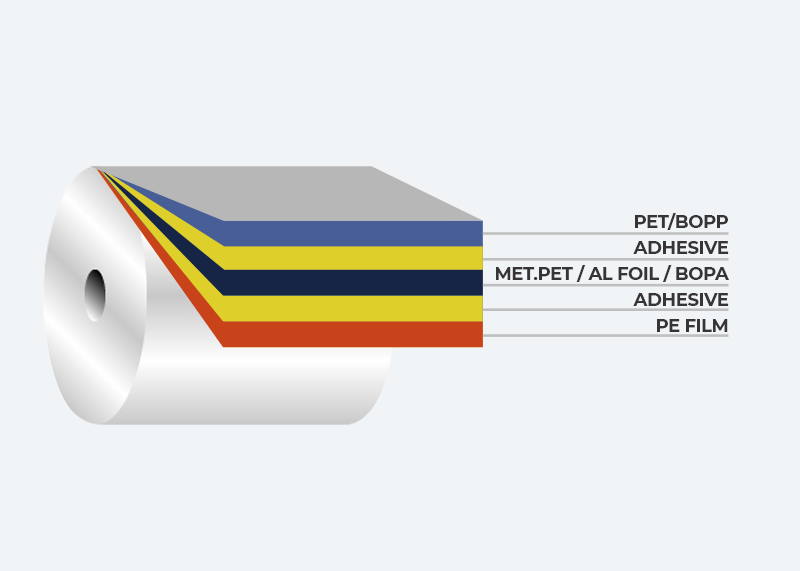
The visible surface of a coffee pouch is not the whole package. Most high-barrier coffee bags combine multiple webs so that printability, protection and heat sealing can be optimized separately.
The correct question is not simply “kraft or foil?” It is “what is the complete layer order, what job does each layer perform, and what evidence supports the finished construction?”
The four functional zones
| Zone | Common direction | Primary job | Risk if poorly specified |
|---|---|---|---|
| Outer web | PET, BOPP or paper | Print carrier, handling surface, stiffness and visual finish | Scuffing, distortion, weak shelf stance or inconsistent color |
| Ink and coating | Reverse print, white ink, matte or gloss treatment | Protected graphics, opacity and controlled appearance | Low contrast, rub-off, blocked windows or unreadable codes |
| Adhesive and barrier | Adhesive plus VMPET, aluminum foil or coated film | Laminate bond and project-specific oxygen, moisture and light protection | Delamination, poor barrier or a report that does not match production |
| Inner sealant | PE or CPP | Food-contact surface and heat-seal behavior | Leakers, narrow sealing window or incompatibility with filling conditions |
Three common construction directions
PET / VMPET / PE
PET commonly carries reverse printing, VMPET provides the metallized barrier direction and PE provides the food-contact seal layer. This route can support many retail coffee projects, but the actual barrier depends on film grade, metallization, layer gauges, converting quality and test conditions.
PET / AL / PE
Aluminum foil creates a continuous metal layer and is used in Crystavo’s PET/AL/PE (100% Barrier) option. The project must still verify the exact report, foil gauge, converting route, flex exposure, valve installation and finished-pouch seals. “Foil” on a quotation should never stand in for a complete specification.
Kraft / VMPET / PE
The paper layer creates the natural visible surface; it is not normally the primary coffee barrier. The metallized film and sealant inside the paper-facing structure provide the protective and sealing functions. Paper shade, fiber texture, printing and rub resistance should be approved on a physical reference.
Why food-contact documentation is construction-specific
For the United States, the regulatory status of the finished food-contact material depends on the status and intended conditions of use of its individual substances. A generic statement about “food-grade material” is not a substitute for reviewing the actual sealant, adhesive, inks and use conditions.
What to write into the purchase specification
- Layer sequence and nominal thickness direction
- Print side, ink system and surface finish
- Adhesive or lamination route and curing requirements
- Barrier layer and applicable OTR/WVTR report reference
- Food-contact sealant and intended conditions of use
- Valve, zipper, dimensions, seals and approved physical sample
This prevents a common purchasing failure: approving the appearance of one material while receiving a different complete laminate in mass production.
Research notes
Sources & standards
- FDA: determining the regulatory status of food-contact material components
- FDA: food ingredient and packaging terminology
- ASTM D3985-24: oxygen transmission testing
- ASTM F1249-25: water-vapor transmission testing
Technical references explain the decision framework. Final performance and compliance depend on the exact approved construction, test conditions, intended use and destination market.